Engineering change notices are where split-vendor PCBA quietly burns schedule. One shop spins the bare board, a broker ships passives, and a third house owns stencil and placement. Then an ECO lands in three inboxes with three revision states, and nobody is sure which kit matches which copper.
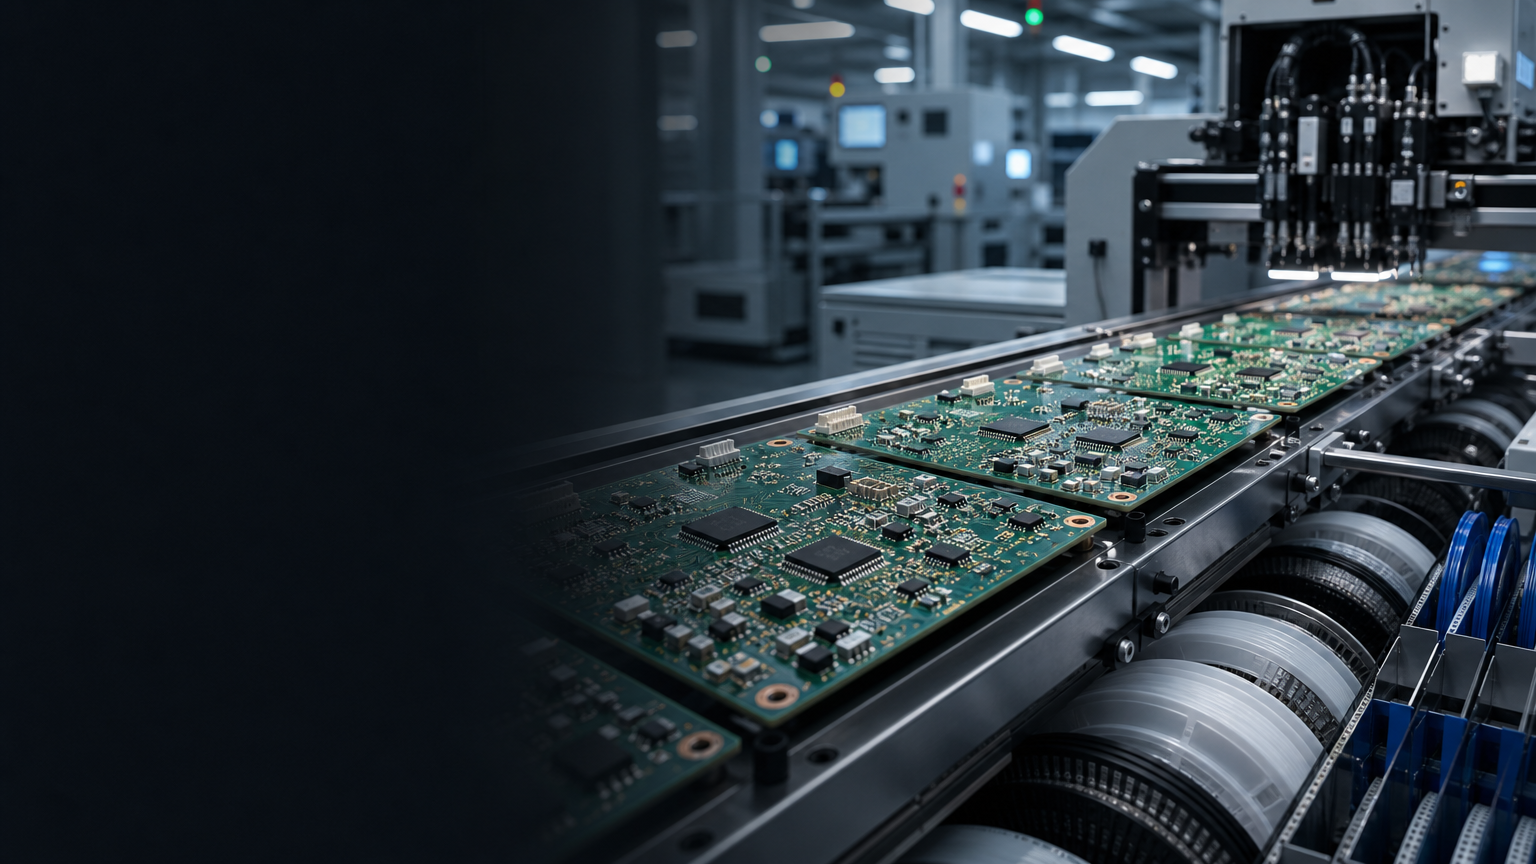
One-stop PCBA exists to collapse that ownership problem. A single manufacturer runs fabrication, sourcing (or coordinated consignment), stencil, SMT/THT, inspection, and delivery under one revision ledger. For overseas teams sourcing from China, the advantage is rarely "magic cheaper parts." It is fewer mismatched date codes, fewer wrong alternates, and fewer stencil revisions that lag the PCB spin.
What one-stop actually centralizes
In a full turnkey model you send design files and requirements; the manufacturer purchases materials, builds the PCB, assembles, tests as agreed, and ships. Partial turnkey keeps critical ICs consigned while passives and commodity parts are purchased. Both can work. Both need a clear owner for the revision package that ties copper, BOM, and stencil together.
Split sourcing can still look cheaper on paper. The landed cost story changes when you count logistics, idle line time waiting for one missing reel, and scrap from assembling the wrong PCB revision to an old BOM.
Where buyers feel the difference
Procurement complexity drops when one purchasing team owns AVL rules, shortage substitutions, and incoming QC. Inventory sitting in your warehouse shrinks because the assembler stages kits against the build schedule. Small-batch and prototype runs become easier because the same owner can absorb low MOQ pain across multiple jobs instead of forcing you to negotiate five suppliers for fifty boards.
Quality and delivery become more predictable when paste lot, PCB lot, and component lots can sit on one work-order genealogy. That matters for industrial, medical-adjacent, and automotive-grade programs even when you are not asking for full PPAP theater.
Startups and lean engineering teams gain flexibility: quantities can move between EVT and pilot without rebuilding a multi-vendor choreography every time the BOM changes.
What one-stop does not automatically fix
A single owner does not replace a complete BOM, usable CPL, or written do-not-substitute flags on firmware-critical ICs. It also does not make an undefined test plan suddenly comprehensive. The commercial win is coordination. The engineering win still depends on files and acceptance criteria.
Automation and process control inside a capable PCBA house help yield, but you should still name SPI, AOI, X-ray, and functional test expectations in the RFQ. "One-stop" is an ownership model, not a substitute for a quality plan.
Choosing the model for your next build
Use one-stop when hardware iterates quickly, ECO bandwidth is thin, or stencil/PCB/BOM revisions must stay locked. Keep partial consignment when you already hold controlled ICs or long-lead ASICs. Dual-source later if needed, but freeze notes and acceptance criteria during the NPI phase first so volume does not rediscover process lessons.
For overseas buyers evaluating full turnkey PCB assembly, ask how ECO numbers propagate across fab and assembly work orders, how substitutions are approved, and what traceability (board serial, date code, reel lot) is delivered. Those answers predict schedule risk better than a unit-price spreadsheet alone.
If component purchasing support is part of the pitch, review components purchasing services expectations against your AVL before the first kit is bought.